

 English
-
01

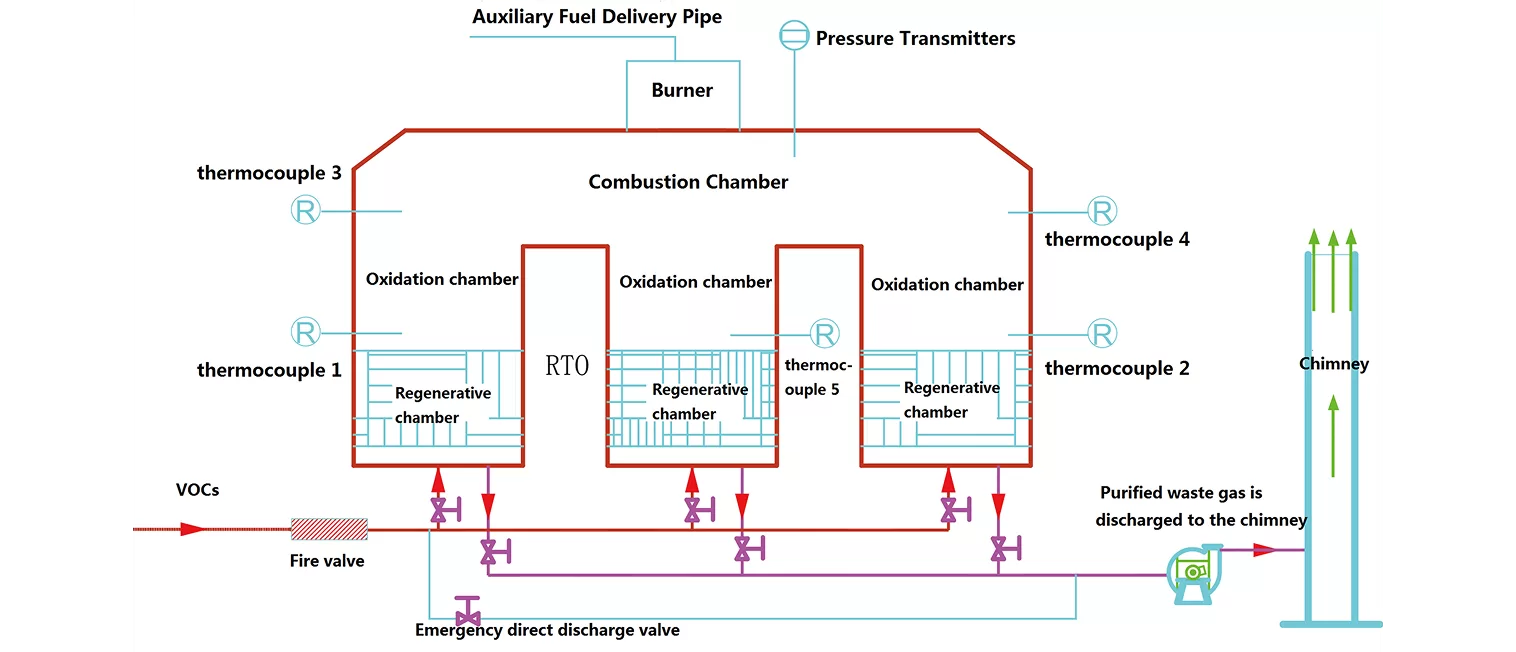
High purification efficiency
VOC removal rate is typically over 99%.
-
02

Extremely high thermal efficiency
Heat recovery efficiency can reach 90% to 95%.
-
03

Energy and fuel efficient
Utilizes residual heat for preheating at high temperatures, significantly reducing energy consumption
-
04

Low operating costs
Daily operation, maintenance, and fuel costs are low.
-
05

High safety performance
Equipped with multiple explosion-proof and safety control systems.
-
06

Automated Control
Fully automatic PLC operation; simple to operate and manage.
| Model | Air Flow(m3/h) | Size (mm) | Burner Demand |
|---|---|---|---|
| 3T-RTO-005 | 5000 | 5570*2070*4900mm | 25*104kcal |
| 3T-RTO-010 | 10000 | 7170*2370*5000mm | 25*104kcal |
| 3T-RTO-015 | 15000 | 8520*2670*5200mm | 55*104kcal |
| 3T-RTO-020 | 20000 | 9230*2990*5400mm | 75*104kcal |
| 3T-RTO-030 | 30000 | 11960*2990*5900mm | 100*104kcal |
| 3T-RTO-050 | 40000 | 14720*2990*6400mm | 135*104kcal |
| 3T-RTO-100 | 50000 | 17450*2990*7000mm | 200*104kcal |
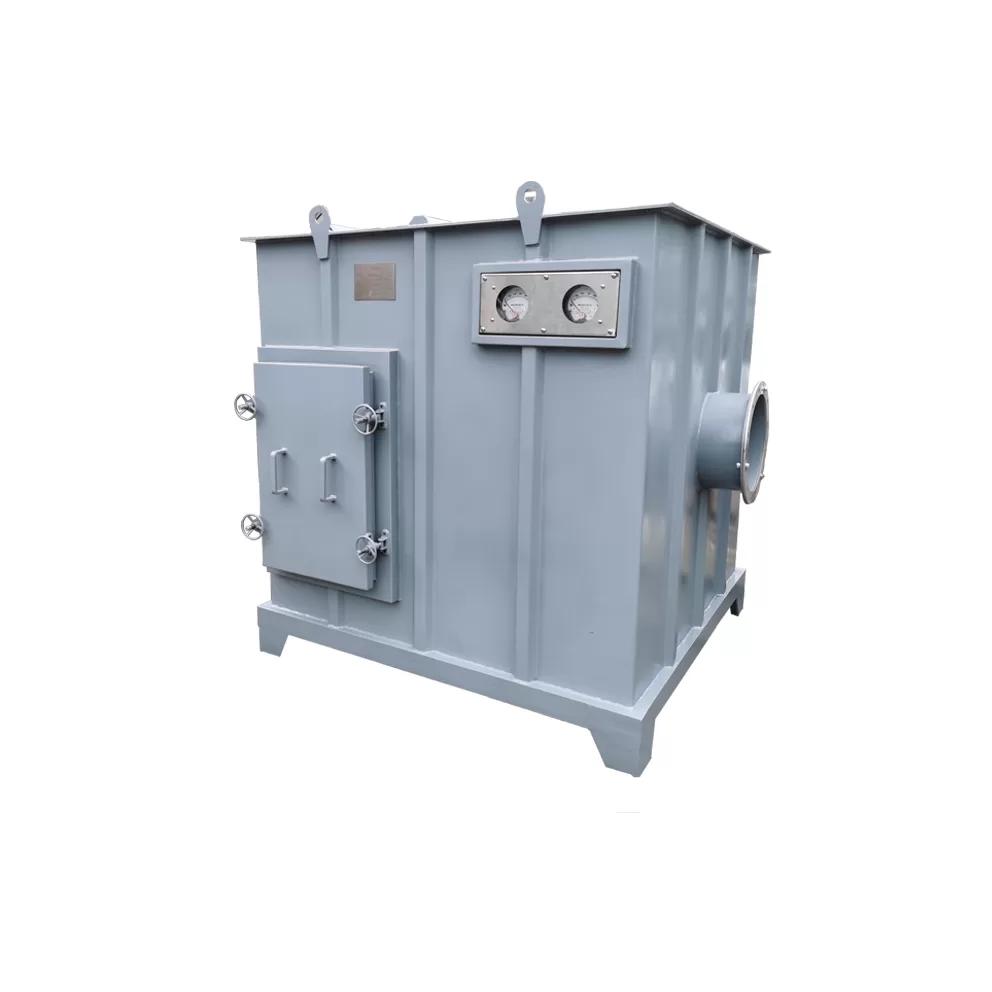
Inlet Air Filtration Unit
Filtration of paint mist during equipment painting processes;Dust filtration at workshop fresh air intakes;Dust and mist removal upstream of rotary concentrators and downstream of scrubbing towers;Filtration and capture of particulates in industries such as petroleum, pharmaceuticals, and chemicals.
 Explore More
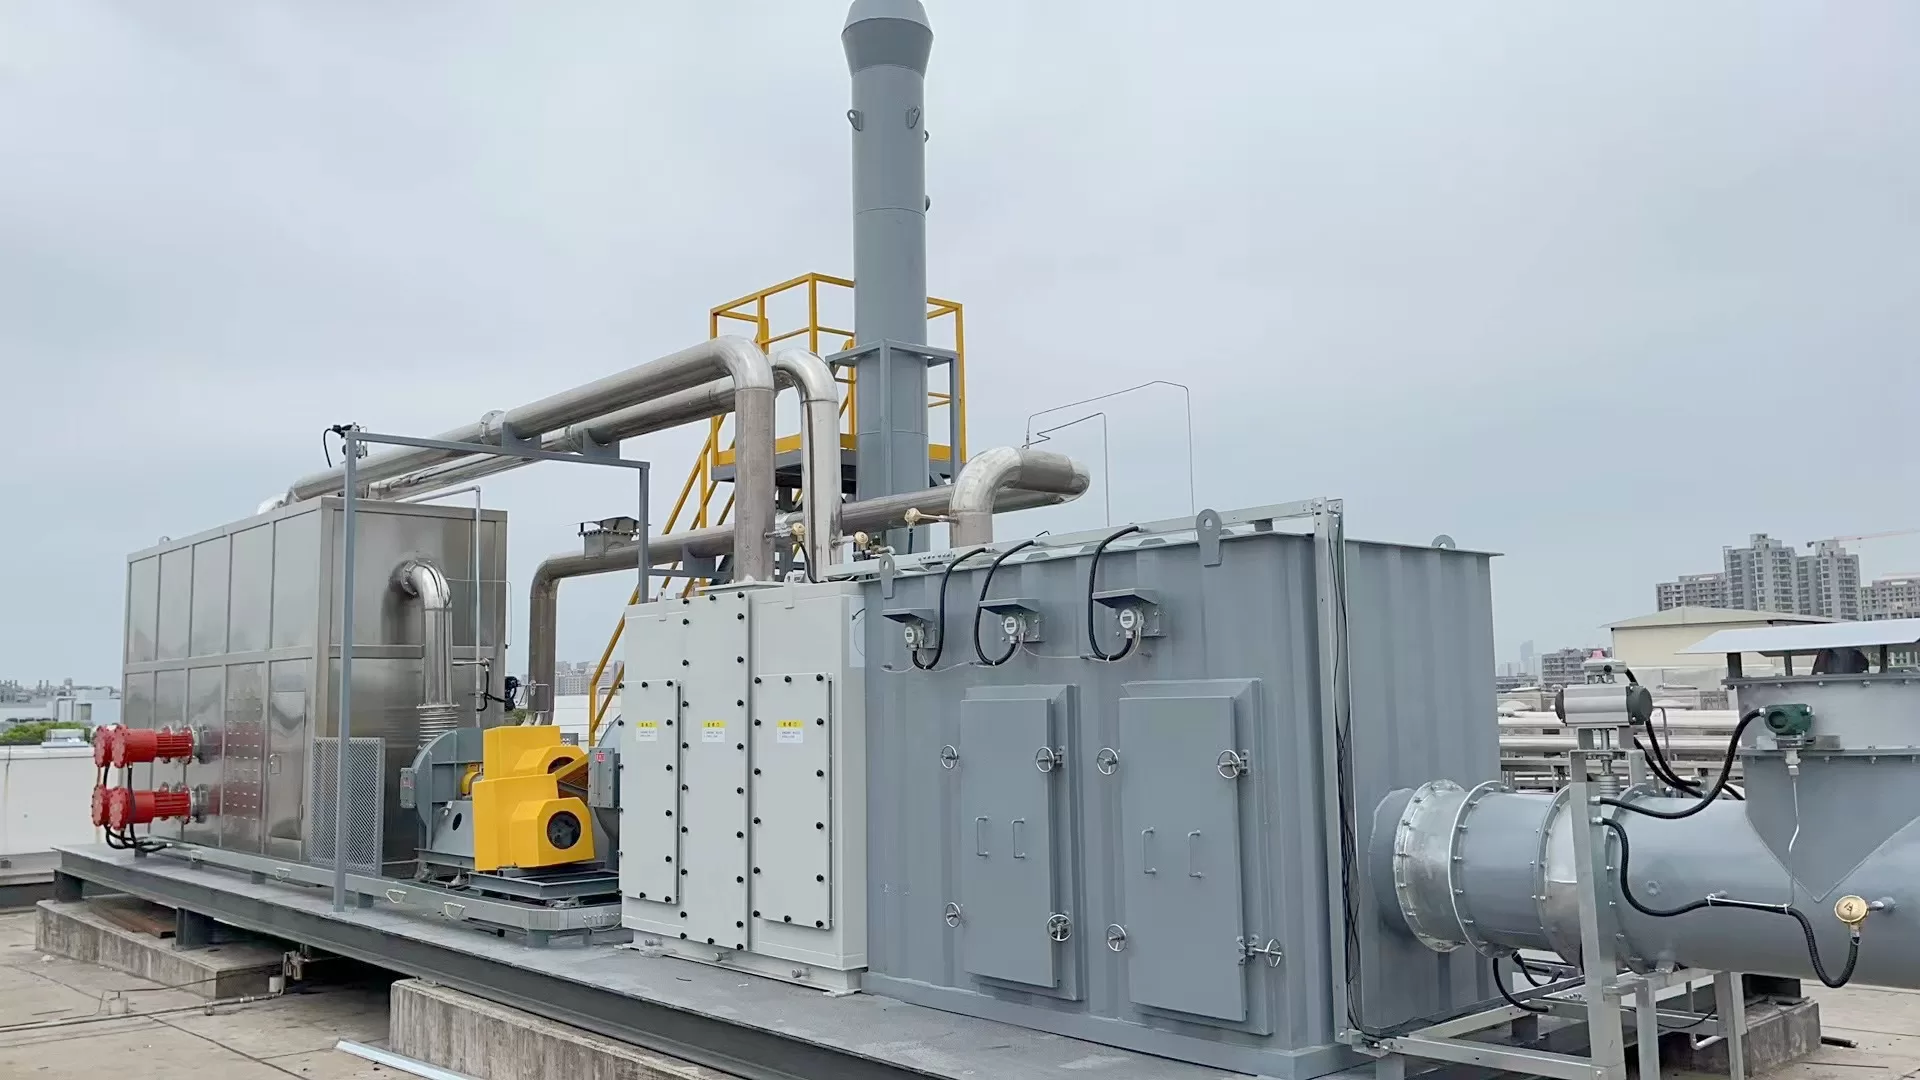
Zeolite Concentration Rotor + Catalytic Combustion (CO) System
The zeolite concentration rotor and catalytic combustion (CO) system is primarily used in industries such as spray painting, printing, coatings, automotive painting, ink printing and dyeing, papermaking, injection molding, coating processes, electronics manufacturing, and the chemical industry.
Explore More
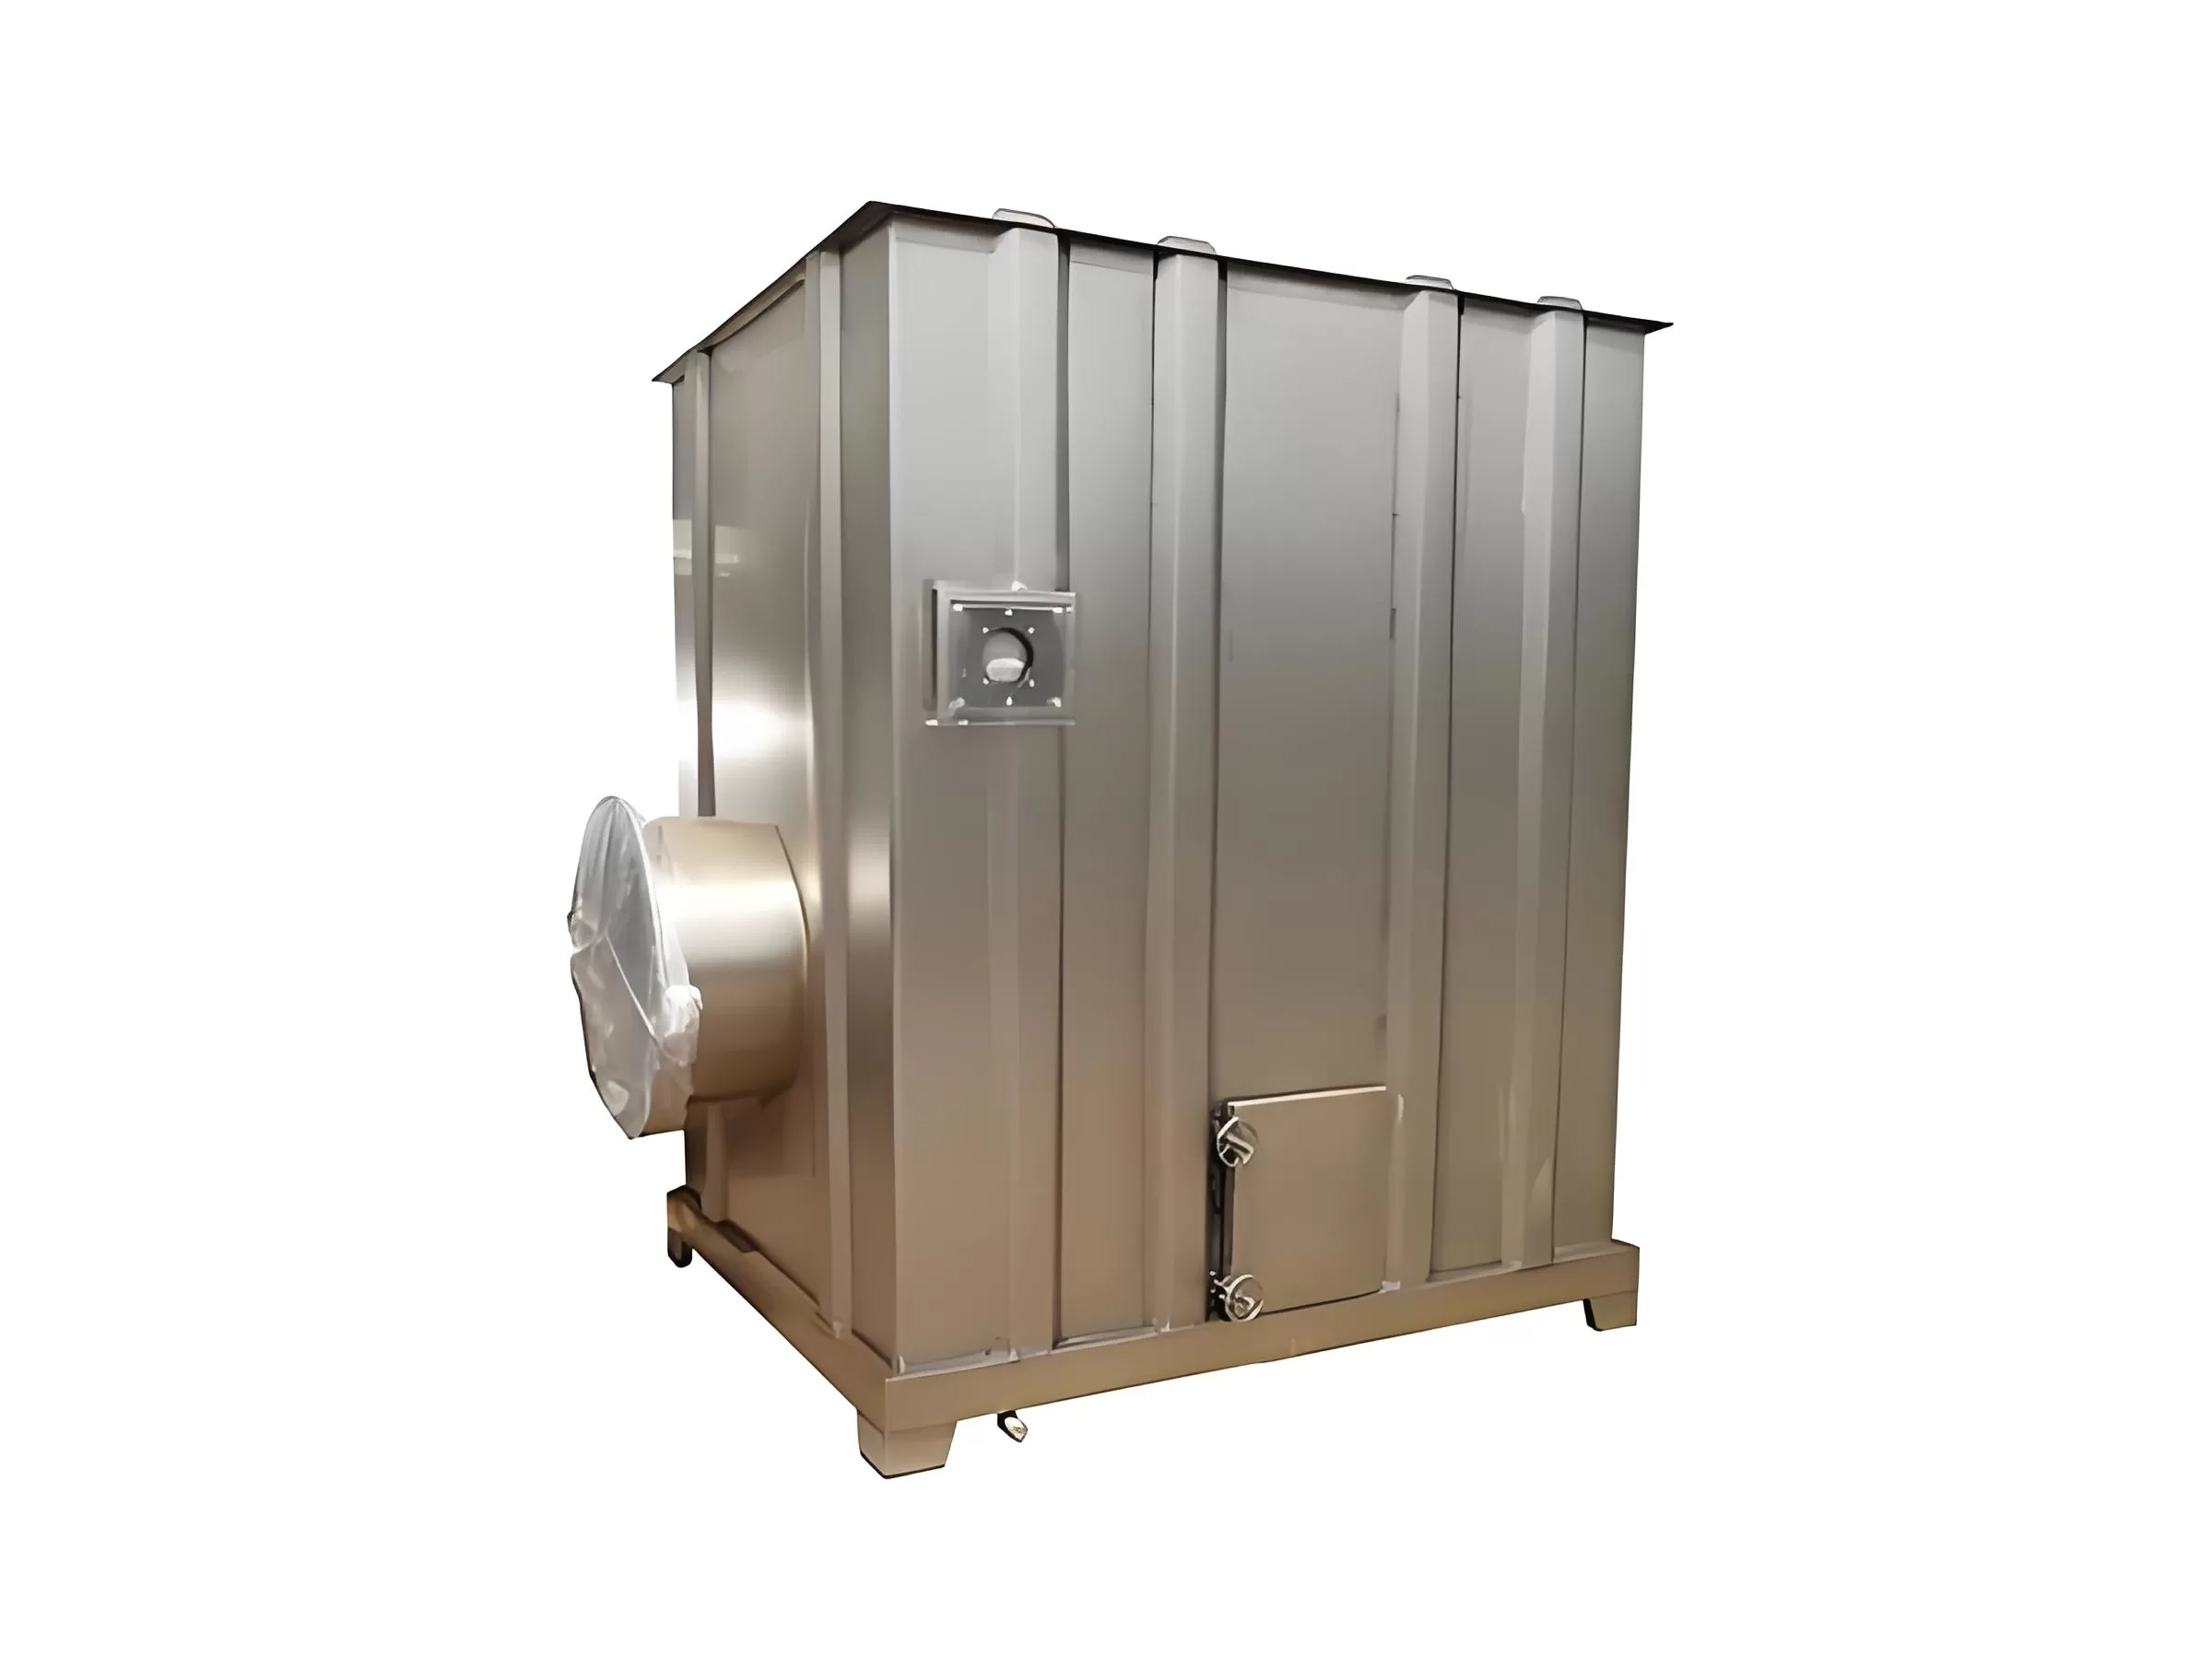
Activated Carbon Filter (ACF)
Activated carbon adsorption units are primarily designed to treat various organic and inorganic pollutants—including benzene, ketones, alcohols, ether, alkane, mixed organic waste gases, as well as acidic and alkaline exhaust gases. They are suitable for the purification of harmful exhaust gases generated in sectors such as pharmaceuticals, metallurgy, chemicals, machinery, electronics, electrical appliances, coating, footwear, rubber, plastics, and printing, as well as for environmental applications involving desulfurization and deodorization in various industrial production workshops.
Explore More
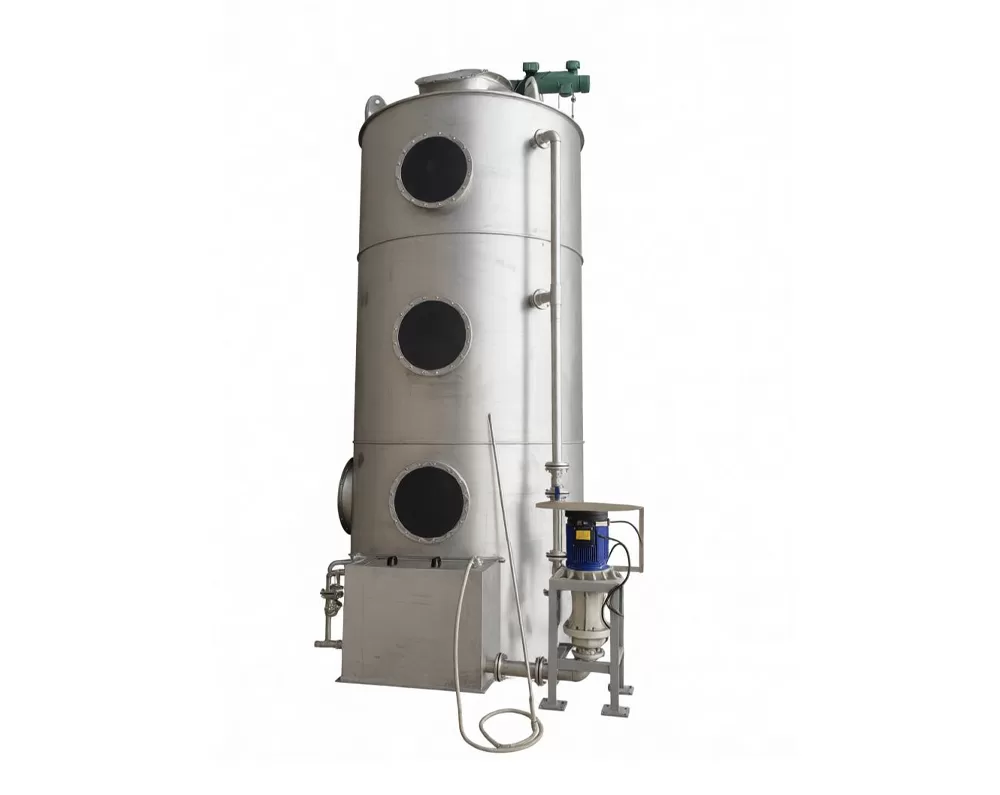
Scrubber
Stainless steel scrubbing towers are available in single-tower and dual-tower configurations. They typically consist of a liquid storage tank, tower body, air inlet section, spray layer, packing layer, cyclonic mist eliminator layer, exhaust cone cap, and access manholes. They are primarily used to treat various harmful gases, such as H₂S, SOₓ, NOₓ, HCl, NH₃, and Cl₂.
Explore More
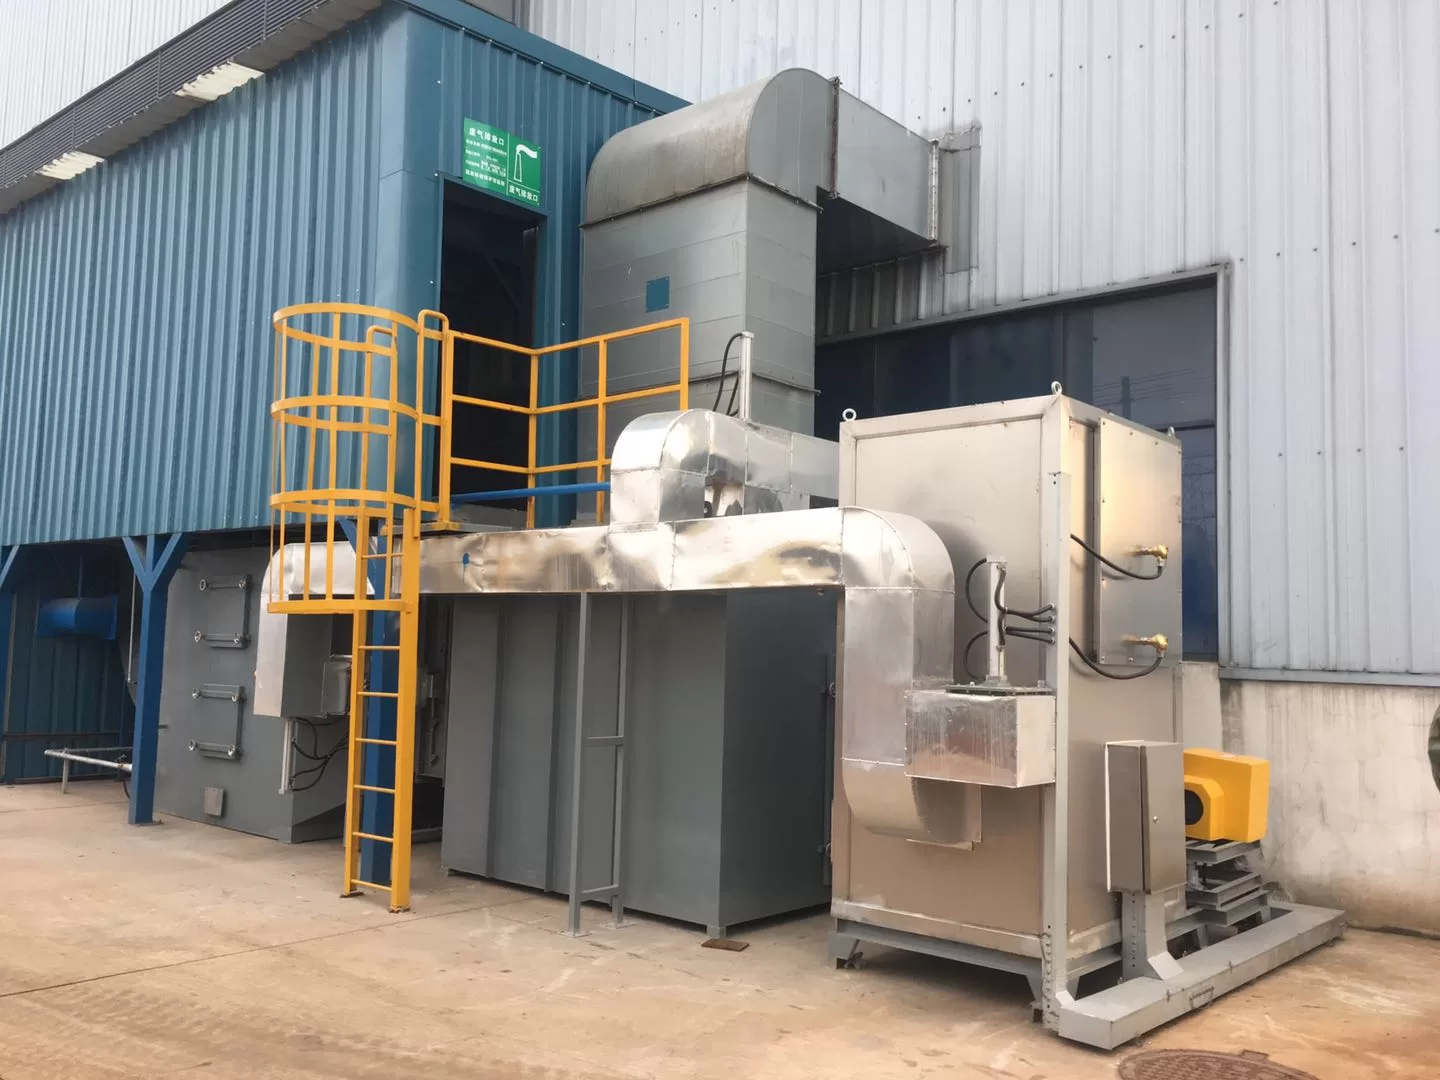
Catalytic oxidizer(CO)
The catalytic purification unit primarily consists of a housing, a heat exchanger, an electric or burner-based heating system, a catalytic bed, and a control system. The various components operate with interlocked controls, ensuring stable performance.
Explore More
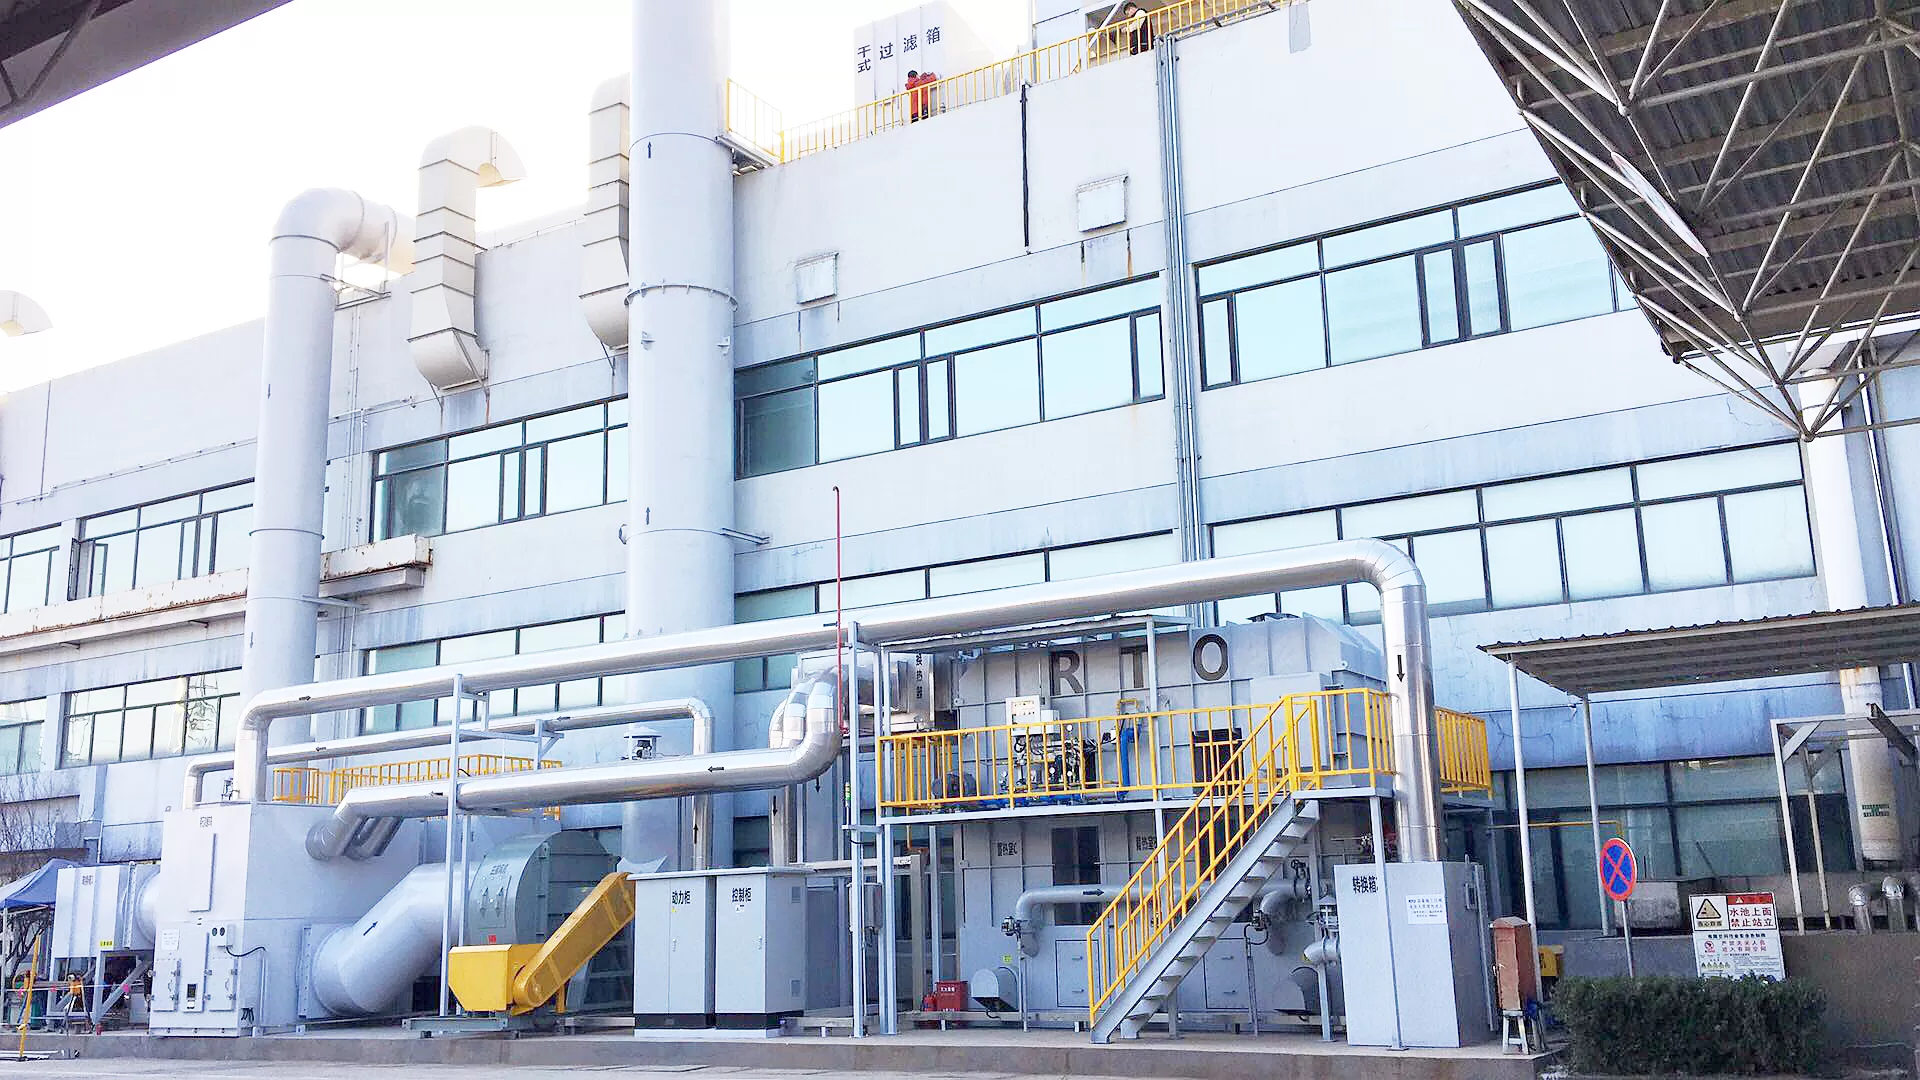
Zeolite Concentration Rotor + Regenerative Thermal Oxidizer (RTO)
The zeolite concentration rotor + Regenerative Thermal Oxidizer(RTO) system is suitable for treating low-concentration, high-volume organic waste gas. The system primarily consists of a pre-treatment unit, a zeolite concentration rotor, an RTO unit, a fan, and a stack.
Explore More
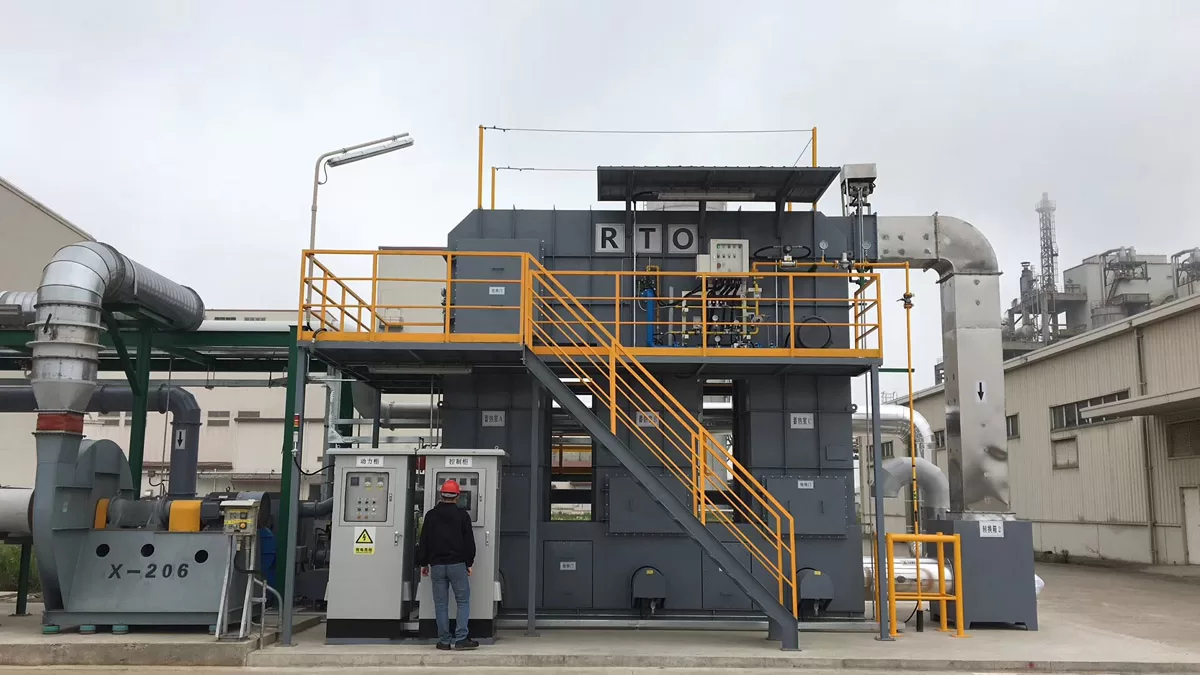
Regenerative Thermal Oxidizer (RTO)
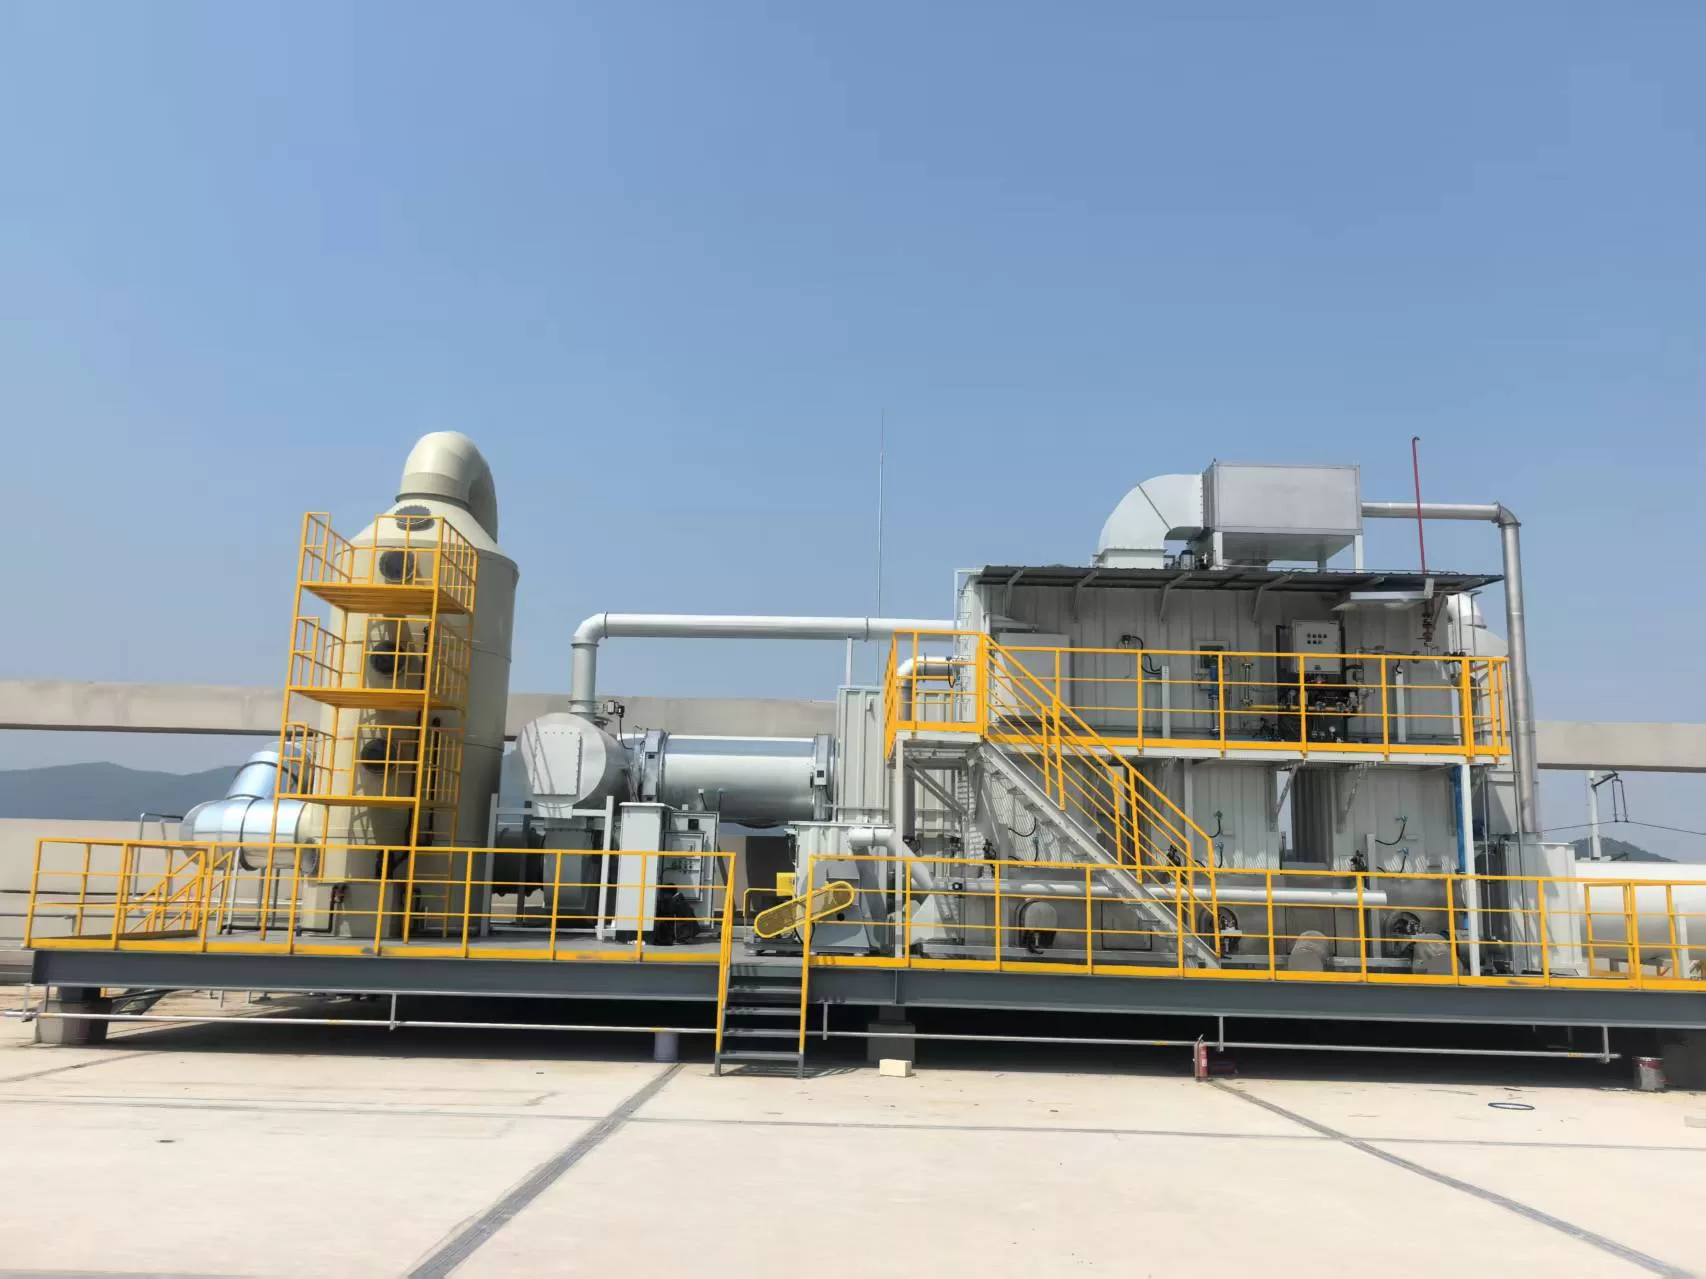
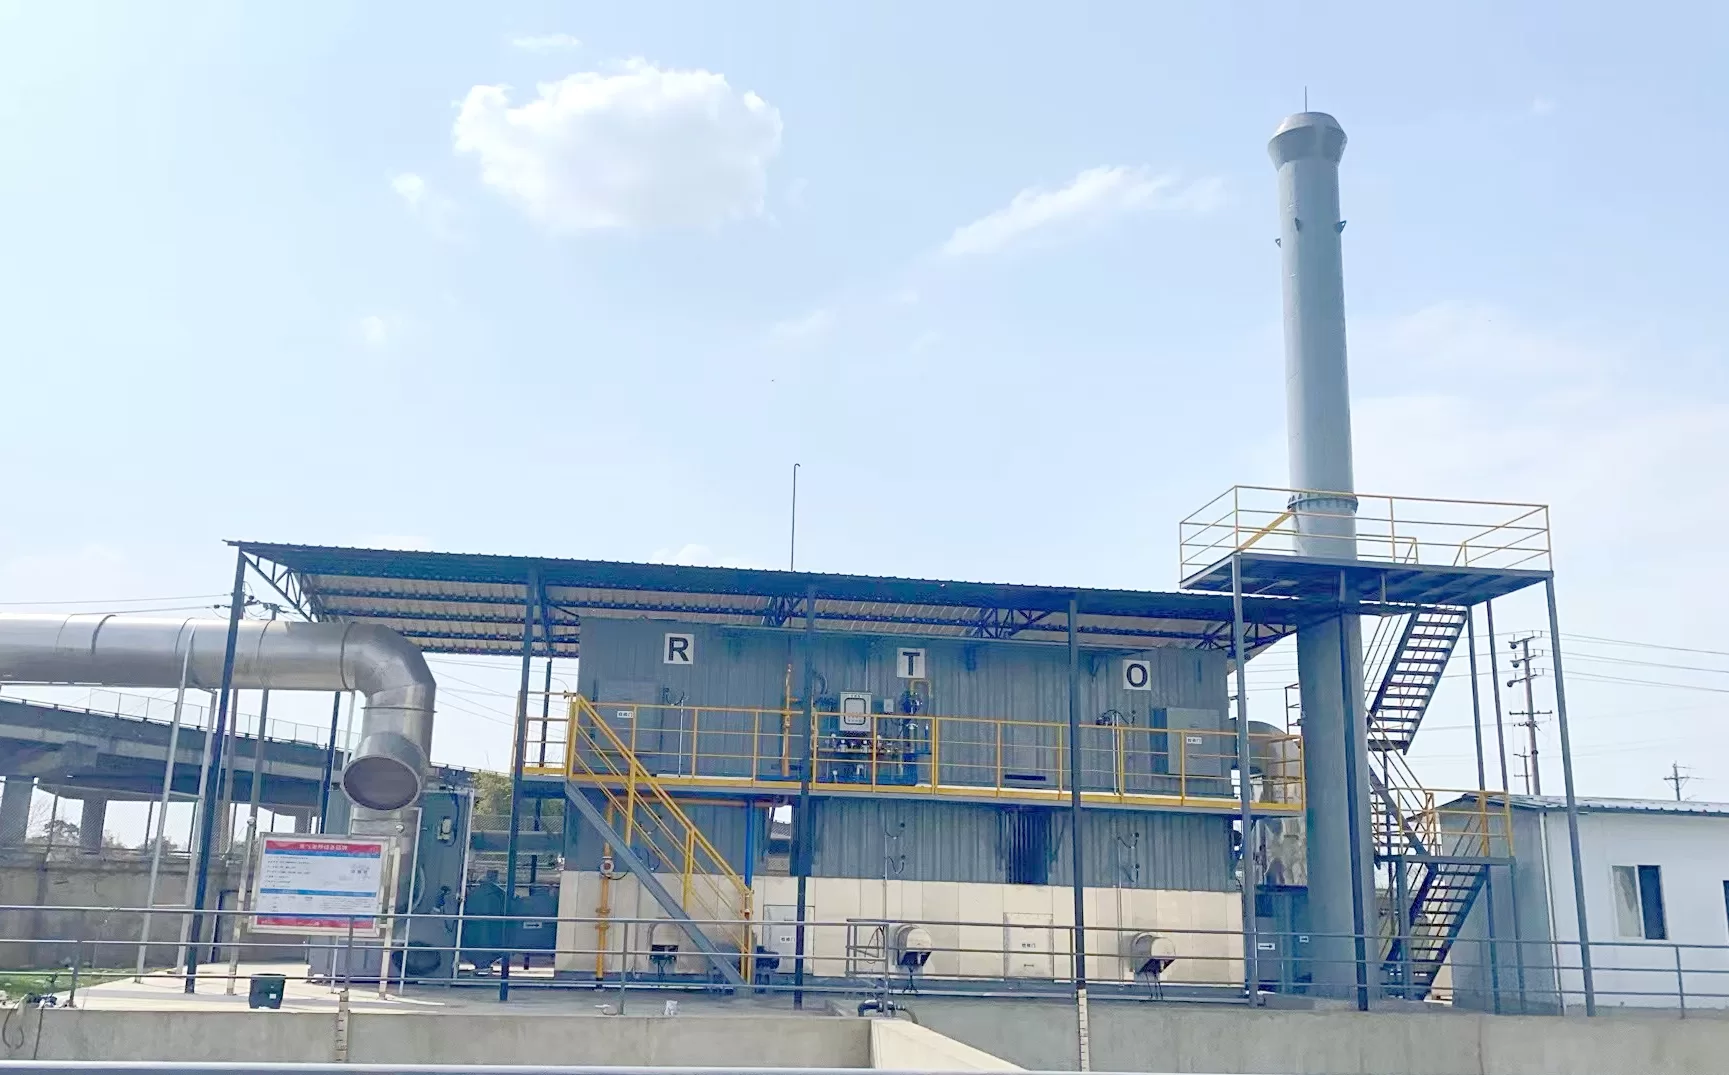
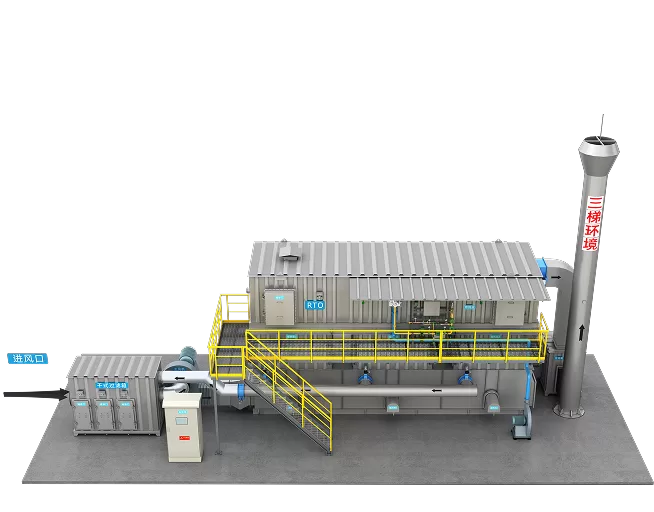
The Regenerative Thermal Oxidizer (RTO) primarily consists of a heat storage chamber, an oxidation combustion chamber, switching valves, a burner, gas supply and combustion-supporting systems, a compressed air system, and a control system. The operation of these components is interlocked, ensuring stable performance.
Explore More
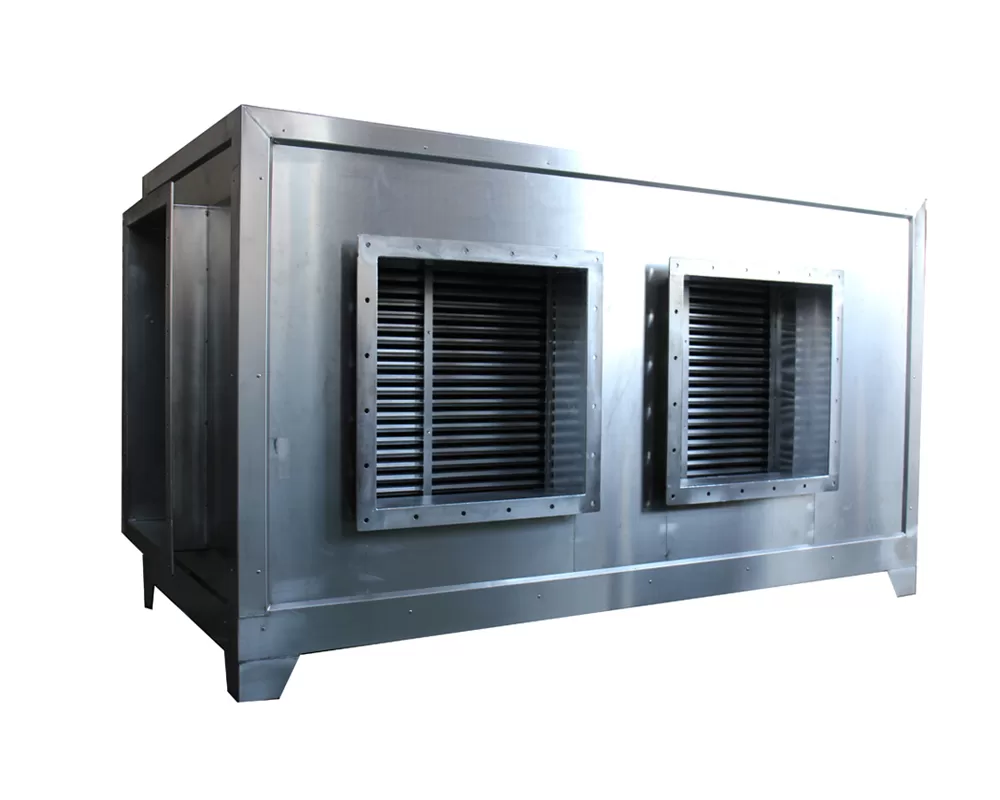
Plate Heat Exchanger(gas to gas)
Gas-to-gas plate heat exchangers are primarily used in conjunction with exhaust gas treatment systems—such as Regenerative Thermal Oxidizer (RTO) and Catalytic Oxidation (CO) systems—and are suitable for air preheating and waste heat recovery applications in industries including iron and steel, papermaking, chemicals, power generation, and battery manufacturing.
Explore More


Need a VOCs Treatment Solution?
Talk with our engineering team about your process, airflow and emission targets.

 Oxi.X - Thermal processes